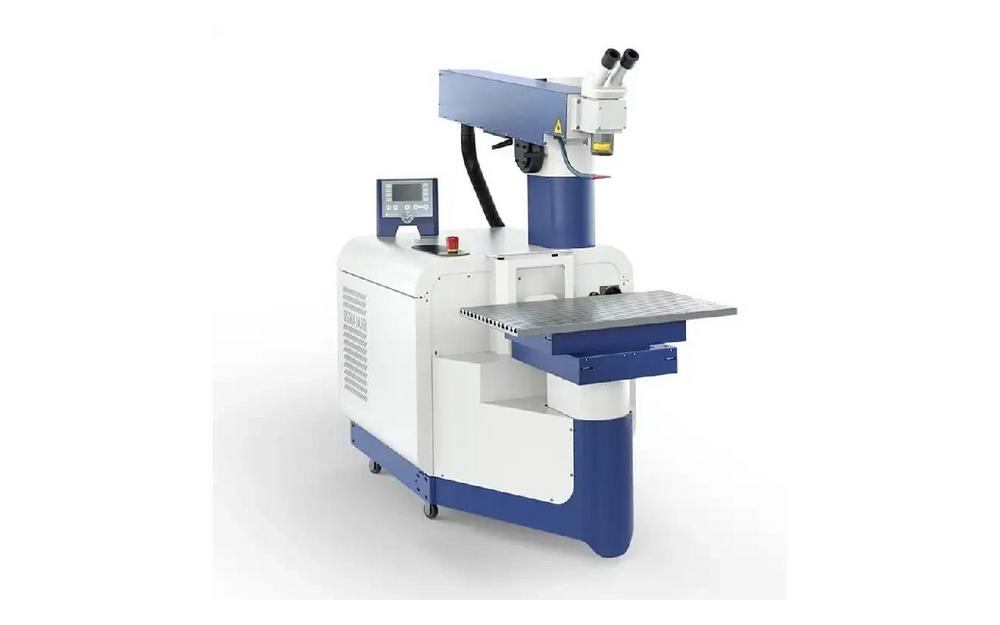
Most defects are local and can be welded in place
Damage on injection moulds and die-casting dies is usually confined to specific areas. The main groups are:
- Edges: chipped or worn parting-line edges, worn sealing and shut-off edges, worn radii and corners
- Cracks: heat-checking cracks on die-casting surfaces (surface only), short cracks at edges
- Erosion and pitting: erosion and pitting from the melt, local surface loss
- Seats and dents: damaged ejector or insert seats, dents from handling
Nearly all of these can be repaired by laser build-up welding directly on the tool. Only through-cracks that run across the entire insert require a new part. For all others, material is added exactly where needed and the tool remains in one piece.
Laser build-up welding restores the surface without affecting hardness or dimensions
Laser build-up welding adds filler wire, matched to the tool steel, at the precise spot indicated by the microscope cross-hair. The process uses pulse energy up to 170 J and peak power up to 13 kW, allowing controlled melting of the filler without significant heating of the surrounding steel. This keeps the tool’s hardness and dimensions intact. Mobile five-axis workstation systems are brought to the mould, whether in the toolroom or next to the press. Swivelling optics reach undercuts and deep cavities, so most repairs do not require dismantling or transport of the tool.
The steel grade decides how the repair is done
The first step in any repair is to identify the steel grade, such as 1.2344 (H13) or 1.2343, and its heat treatment. Filler wire, pulse shape and any pre-heating are chosen to match the material. High-carbon tool steels are prone to cracking under heat.
Super Pulse Technology shapes the pulse to keep the heat-affected zone small, allowing even these steels to be welded without cracks.
“In the toolroom people judge a defect by how it looks, but the steel decides the route. I have seen two defects that looked identical and needed completely different settings,” says Alexander Bellouzi, Senior Design & Engineering at Sigma Laser.
What that means for the production schedule is covered in the article on how fast a repaired mould is back in production, and a sample weld on your own tool steel settles the repair route before the first real job.
Sigma Laser has developed and manufactured industrial laser welding systems in Hanau, Germany, since 2005. The range comprises six five-axis systems – mobile (Sineo Light, Sineo Fibre, Sirius Light) and stationary (Sidanus Light, Sidanus Fibre, Siega Fibre) – with Nd:YAG (1064 nm) or fibre laser sources (1070 nm), complemented by Simass automation modules and Super Pulse Technology. The Sineo system won the German Design Award 2025; customers are located in more than 25 countries.
Sigma Laser GmbH
Pfaffenbrunnen Str. 158
63456 Hanau-Steinheim
Telefon: +49 (0)6181 413 6679
https://sigma-laser.com
